
 Business License
Blog Categories
Flame Temperature and Gas Pressure Specifications for Torches
Two torches with the same headline flame temperature can behave quite differently on the bench, because the second figure on the sheet is the pressure they are set to run at.
This article covers the torch flame temperature spec and what it really measures, the gas torch pressure rating at the inlet and at the tip, and the brazing torch heat output that decides how fast a joint reaches temperature.
1. Torch Flame Temperature Spec: How the Figure Is Stated
A torch flame temperature spec is usually quoted as the hottest point the flame can reach, and that point is not where the work sits.
The peak figure comes from the primary flame zone, the bright inner cone just past the tip, where combustion is complete and the gas is fully reacted.
The work sits a little beyond that zone. Placing the cone on the joint gives the highest heat transfer, while a larger gap lets the flame cool in the air.
Temperature also depends on the oxidiser. The same fuel gives a much hotter flame in pure oxygen than it does in the air drawn in around the burner.
A spec sheet that quotes a single number without saying air or oxygen is describing an upper limit rather than a working figure.
For a buyer the useful reading is the pair: the fuel, and whether the burner draws its oxygen from the air or from a cylinder.
Some sheets quote an adiabatic figure, the temperature a flame would reach with no loss at all. That number is higher than any measured flame and is not the figure to plan a joint from, though it still turns up in older catalogues.
2. Gas Torch Pressure Rating: Inlet and Working Pressure
A gas torch pressure rating covers two different numbers, and confusing them is a common reason a torch runs below its expected heat output.
The first is the cylinder or inlet pressure, which is set by the fuel itself and by the temperature of the cylinder on the day.
Propane holds a vapour pressure of roughly 8 bar at 20 °C, and that figure falls as the cylinder cools through a long job.
The second is the working pressure at the burner, which is set by a regulator on a hose torch or fixed by the jet on a body-mounted torch.
An air fuel burner with no regulator runs on cylinder pressure through a fixed jet. That keeps the set simple and sets the flame by jet size rather than by a dial.
A hose torch with a regulator lets the outlet be held steady, which keeps the flame constant even as the cylinder pressure falls across the shift.
3. Brazing Torch Heat Output: Heat Into the Joint
Brazing torch heat output is the figure that decides how long a joint takes to reach temperature, and it is quoted in power rather than in degrees.
The usual unit is the kilowatt, sometimes written as kilojoules per hour, where 1 kW is 3,600 kJ per hour.
A single-tip air fuel burner typically puts out about 1.5 kW to 3 kW, depending on the gas and the tip size fitted.
A multi-tip head multiplies that figure by the number of tips, which is why a triple-tip torch warms a large fitting far faster than a single tip.
Not all of that output lands in the work. A share is lost to the surrounding air, and a larger share is drawn away by the mass of the fitting itself.
The honest figure for planning is heat into the joint, which is why a thick casting needs a larger burner than a thin tube of the same diameter. Wentu lists the heat output of each burner against the tip size it was measured with, so the figure can be compared across the range.
Time follows from the same arithmetic. A joint that needs 2 kJ of useful heat takes about two seconds from a burner delivering 1 kW to the work, and considerably longer once the metal around it starts to draw heat away.
4. Torch Flame Temperature Spec: Air Fuel and Oxy Fuel
The torch flame temperature spec moves across a wide range once the oxidiser changes, and the table below sets out the common pairings.
Propane burning in air reaches about 1,927 °C. That covers soft soldering, thawing and light heating on copper and steel.
MAPP gas burning in air reaches about 2,926 °C, close to the top of what an air torch can produce without an oxygen supply.
Adding pure oxygen lifts both fuels well above their air figures. Oxy-propane reaches about 2,800 °C and oxy-acetylene about 3,160 °C.
The table sets the four common flames side by side on the figure a bench buyer compares.
| Fuel and oxidiser | Flame temperature | Typical work |
|---|---|---|
| Propane in air | about 1,927 °C | Soft soldering, light heating |
| MAPP in air | about 2,926 °C | Brazing copper lines |
| Oxy-propane | about 2,800 °C | Heavier brazing, light welding |
| Oxy-acetylene | about 3,160 °C | Welding and cutting |
The table also shows why an air fuel set stays popular on repair benches, since it reaches brazing temperature with one cylinder and no oxygen line.
5. Gas Torch Pressure Rating: Regulators and Hoses
A gas torch pressure rating depends on the regulator and the hose behind it, because both sit between the cylinder and the flame.
A regulator holds the outlet at a set pressure and absorbs the fall in cylinder pressure as the fuel is drawn down.
A typical outlet setting for brazing work sits in the range of about 0.5 bar to 2 bar, adjusted to the tip and the fuel in use.
A two-gas set carries a separate regulator for each line, so oxygen and fuel are set independently rather than sharing one outlet.
The hose has to be rated for the pressure and the fuel. An unrated line can harden, crack and leak, which is a fault that appears at the fittings first.
A flashback arrestor at the torch end of each line is standard practice on a set used daily, since it stops a flame travelling back down the hose.
Wintooltech states the working pressure for each burner at the tip rather than at the cylinder, so the figure can be checked against the regulator setting on the bench. Wentu supplies the matching regulator where a buyer needs the whole line set as one system.
6. Brazing Torch Heat Output: Matching a Torch to a Joint
Brazing torch heat output is chosen from the joint, not from the torch catalogue, and the joint sets a heat input that has to be reached and held.
Soft soldering on a copper pipe needs about 200 °C at the joint and takes a small propane flame without difficulty.
Brazing a copper line needs 600 °C to 800 °C at the work, which a MAPP flame reaches faster than propane on the same tip size.
Mass changes the answer. A thick fitting draws heat away from the joint, so a burner that suits a thin tube can struggle on a heavy valve body.
Position matters as much as output. Holding the cone about 15 mm from the work puts the hot zone on the joint, while a wider gap wastes heat into the air.
Where a joint is close to a sensitive part, a smaller tip held longer usually beats a large tip used quickly, since the heat stays local.
7. Torch Flame Temperature Spec: Measuring at the Work
A torch flame temperature spec describes the flame, while the number that matters on site is the temperature the joint actually reaches.
That figure is lower than the flame figure for two reasons. Heat is lost to the air, and heat is conducted away into the metal around the joint.
A contact thermometer or a thermal marker on the work gives the practical answer, and it costs far less than a bad joint discovered later.
The reading is taken at the joint rather than at the flame, and it is taken with the torch held in the working position. A figure taken with the burner lying on the bench says nothing about how the flame behaves in the hand.
The gap between flame and work temperature also explains why two torches with the same spec can perform differently in the field.
A burner that holds the cone steady on the joint delivers more useful heat than a hotter flame waved across the fitting.
Wintooltech quotes its burners on gas type, tip size and working pressure together, so the flame figure is read alongside the conditions it was measured at.
8. Gas Torch Pressure Rating: Reading a Spec Sheet
A gas torch pressure rating is the line most often misread on a spec sheet, so it is worth knowing what each column is telling the buyer.
The fuel column names the gas the burner is set for, since a jet sized for propane will not give the same flame on MAPP.
The pressure column states the working pressure at the burner, not the pressure inside the cylinder.
The tip column gives the range the burner can accept, usually as a set of tip sizes or a single size, and it sets the flame width.
The duty column gives the continuous working period, which matters on a bench that runs a torch for hours at a time.
Yichun Wentu Imp&Exp Trade Department lays out its torch sheets on those four columns, and Wentu supplies the matching regulator and hose with the burner on request.
A sheet that lists gas, pressure, tip and duty on one page saves a call. A buyer can compare two burners against the same four columns, and the choice usually becomes clear without a trial run.
9. Frequently Asked Questions on Brazing Torch Heat Output
9.1 How should a torch flame temperature spec be read?
A torch flame temperature spec should be read as the peak temperature in the primary flame zone, not as the temperature at the joint. The figure applies at the bright inner cone just past the tip, where combustion is complete, so the work is placed a little beyond it. The same fuel gives a much hotter flame in pure oxygen than in the air drawn in around the burner, which is why a spec should state the oxidiser. Propane in air reaches about 1,927 °C and MAPP in air about 2,926 °C, while oxy-acetylene reaches about 3,160 °C.
9.2 What does a gas torch pressure rating refer to?
A gas torch pressure rating covers two separate numbers, the inlet pressure at the cylinder and the working pressure at the burner. Propane holds a vapour pressure of roughly 8 bar at 20 °C, and that figure falls as the cylinder cools through a long job. The working pressure is set by a regulator on a hose torch or fixed by the jet on a body-mounted torch, with a typical brazing setting around 0.5 bar to 2 bar. Confusing the two is a common reason a torch runs below its expected heat output.
9.3 What heat output does brazing work need?
Brazing torch heat output is quoted in kilowatts, and a single-tip air fuel burner typically puts out about 1.5 kW to 3 kW depending on the gas and the tip fitted. A multi-tip head multiplies that figure by the number of tips, which is why a triple-tip torch warms a large fitting far faster than a single tip. Not all of the output lands in the work, since a share is lost to the air and a larger share is drawn away by the mass of the fitting. Soft soldering needs about 200 °C at the joint, while brazing a copper line needs 600 °C to 800 °C.
9.4 How are the regulator and hose chosen?
The regulator and hose are chosen to hold the working pressure the burner is set for and to carry the fuel in use. A regulator holds its outlet steady and absorbs the fall in cylinder pressure as the fuel is drawn down, with a typical brazing setting around 0.5 bar to 2 bar adjusted to the tip. A two-gas set carries a separate regulator for each line so oxygen and fuel are set independently. A hose rated for the pressure and the fuel is essential, since an unrated line can harden and crack, and a flashback arrestor at the torch end is standard practice on a set used daily.
Recently Posted
-
Gas Torches in Jewelry Making and Precision Metalwork
October 16, 2026A repair bench once lost a ring setting to a flame that was too large rather than too hot. The torch was a workshop unit meant fo Read More
-
Self Igniting vs Manual Ignition Gas Torches
October 16, 2026A technician on a roof replaced a torch mid job and noticed that the two models weighed the same and lit the same flame, yet one Read More
-
Introduction to Air Fuel Torches: MAPP, Propane and LPG
October 15, 2026A workshop bought a torch for brazing refrigeration lines and found the flame too soft to bring a joint up to temperature. The to Read More
-
What Is a MAPP Gas Torch? Definition and Core Components
October 15, 2026A technician new to refrigeration work once asked why a 22 mm brazed joint that took 20 minutes with a propane torch came togethe Read More

Contact Us
Recommended Products
-
 WT‑SSA Premium Aluminum Housing Self‑Igniting MAPP Torch, 360° Swivel Stainless Tip TorchNegotiableMOQ: 100 Pieces
-
WT‑SST Self‑Igniting Brass Tip MAPP Torch, 360° Swivel Fast‑Cooling Premium Brazing TorchNegotiableMOQ: 100 Pieces
-
WT‑SS Self‑Igniting MAPP Gas Torch, 360° Swivel Stainless Steel Tip High‑Heat Brazing BlowtorchNegotiableMOQ: 100 Pieces
-
WT‑S 360° Swivel Single‑Tip MAPP/Propane Gas Torch, Stainless Steel Tip Manual Ignition Brazing TorchNegotiableMOQ: 100 Pieces
-
WT‑5STA Premium Aluminum‑Handle Pistol‑Grip MAPP Torch Heavy‑Duty Brass‑Tip Welding TorchNegotiableMOQ: 100 Pieces
-
WT‑5ST Pistol‑Grip MAPP Gas Torch With Fast‑Cooling Brass Tip Safety‑Lock TorchNegotiableMOQ: 100 Pieces
-
WT‑5S Ergonomic Pistol‑Grip MAPP Gas Torch Instant‑Ignition Safety‑Lock Brazing TorchNegotiableMOQ: 100 Pieces
-
WH‑DSVP Patented Switchable Dual‑Tip MAPP Hose Torch One‑Hand Needle‑Valve TorchNegotiableMOQ: 100 Pieces
-
WH‑SSVNP Patented Flexible Stainless Tube MAPP Hose Torch All‑Directional Gooseneck TorchNegotiableMOQ: 100 Pieces
-
WH‑DSVAP Patented Switchable Dual‑Tip MAPP Hose Torch Needle‑Valve & Aluminum‑Body TorchNegotiableMOQ: 100 Pieces
-
WH‑DSVA Dual‑Tip MAPP Hose Torch With Needle Valve Self‑Igniting Aluminum Igniter TorchNegotiableMOQ: 100 Pieces
-
WH‑SSVTP Patented One‑Piece MAPP Hose Torch One‑Hand Needle‑Valve & Thick Brass TipNegotiableMOQ: 100 Pieces
-
WH‑SSVT Deluxe MAPP Hose Torch With Needle‑Valve & Thick Brass Tip 6‑Blade Thruster TorchNegotiableMOQ: 100 Pieces
-
WH‑SSV MAPP Hose Torch With Needle‑Valve Flame Adjustment Self‑Igniting Extension TorchNegotiableMOQ: 100 Pieces
-
WH‑SST Self‑Igniting Brass Tip MAPP Hose Torch Fast‑Cooling Extension Brazing TorchNegotiableMOQ: 100 Pieces
-
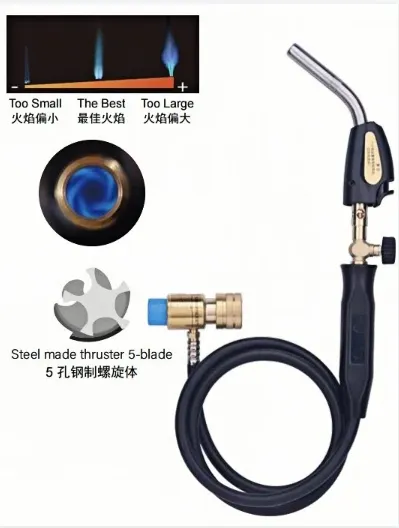
WH‑SS Self‑Igniting MAPP Gas Hose Torch Flexible High‑Pressure Extension Soldering TorchNegotiableMOQ: 100 Pieces
-
WT‑TSA Self‑Igniting Triple‑Tip MAPP Gas Torch Aluminum Housing High‑Heat Brazing TorchNegotiableMOQ: 100 Pieces
-
WT‑T Triple‑Tip Ultra High‑Output MAPP Gas Torch 360° Swivel Three‑Flame Brazing TorchNegotiableMOQ: 100 Pieces
-
WT‑D1SA Premium Self‑Igniting Dual‑Tip MAPP Torch Aluminum Igniter Twin Flame TorchNegotiableMOQ: 100 Pieces
-
WT‑D1A Self‑Igniting Dual‑Tip MAPP Gas Torch 360° Swivel Twin Burner Pipe Welding TorchNegotiableMOQ: 100 Pieces